Mineral Water Bottling Plant
Mineral Water Bottling Plant
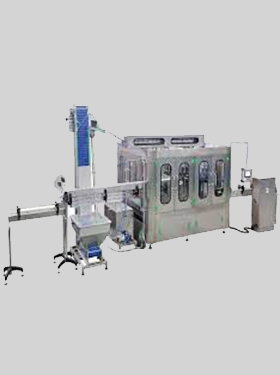
A Mineral Water Bottling Plant is a complete setup designed to purify, process, and package drinking water for commercial sale. Our fully automated plants are ideal for businesses planning to enter the packaged drinking water industry with capacities ranging from 500 LPH to 20,000 LPH.
Process Flow:
Raw Water Intake & Filtration
RO Purification & UV Sterilization
Mineral Addition (as per BIS/FSSAI Standards)
Ozonation for Disinfection
Storage in SS Tanks
Filling, Capping & Labeling (Bottles, Pouches, or Jars)
Plant Components:
Raw Water Treatment System
Reverse Osmosis Plant
Ozonator & UV System
Mineral Dosing System
SS Storage Tanks
Rinsing, Filling & Capping Machine
Conveyor & Labeling Setup
Packaging Equipment (Shrink Wrapping, Carton Sealing)
Available Packaging Options:
200 ml to 2-liter PET Bottles
5-liter & 20-liter Jars
Water Pouches & Sachets
Compliances Covered:
✅ ISI / BIS Standards
✅ FSSAI Certification
✅ Pollution Control Board Guidelines
✅ Complete Documentation & Turnkey Setup
Why Choose Us?
✅ Turnkey Solutions from Design to Installation
✅ High-Speed Filling Machines
✅ Customized Capacity as per Demand
✅ On-Site Setup, Training & AMC Support